Top 10 Profile Projector Machines for Precision Measurement
2026-09-26
When microns matter and every edge tells a story, precision measurement tools become the unsung heroes of the shop floor. Among them, profile projectors stand out for their ability to magnify, inspect, and verify complex geometries with clarity. In this guide, we’ve curated the top 10 profile projector machines that redefine accuracy—and yes, JATEN makes the list for a reason. Whether you're tackling intricate aerospace components or everyday tooling checks, these picks will help you see the difference. Let’s zoom in.
Ten Machines Worth Your Bench Space
A bench is a battleground for space, and every square inch counts. Most tools earn their spot only after proving they can handle more than one type of job. A benchtop bandsaw, for instance, looks bulky at first, but the moment you need to resaw a thin strip or follow a tight curve without burning the wood, you understand why it stays within arm's reach. It's not the flashiest tool in the shop, but it saves time that a jigsaw or handsaw would waste.
Then there's the drill press. If you've ever tried to bore a perfectly vertical hole with a handheld drill and ended up with a wandering bit, you know the frustration. A small benchtop model anchors itself to the corner of the bench, yet it transforms sloppy angled holes into clean, repeatable bores. Pair it with a decent set of brad-point bits, and you'll wonder why you waited so long. A belt and disc sander earns its place too, not as a finishing tool but as a quiet workhorse for truing up edges and shaping small parts that would otherwise clog a bench vise.
For anyone leaning toward smaller-scale work, a miniature wood lathe opens doors that a spindle sander can't. Turning a tool handle or a tiny bowl becomes an evening project instead of a weekend commitment. And if precision carving or inlay work calls, a compact CNC router the size of a toaster oven can mill lettering, pockets, and repeatable joinery without demanding a dedicated room. These machines don't just occupy space; they multiply what you can build on the same bench.
The Spec Sheet Trap: Reading Between Micron Lines
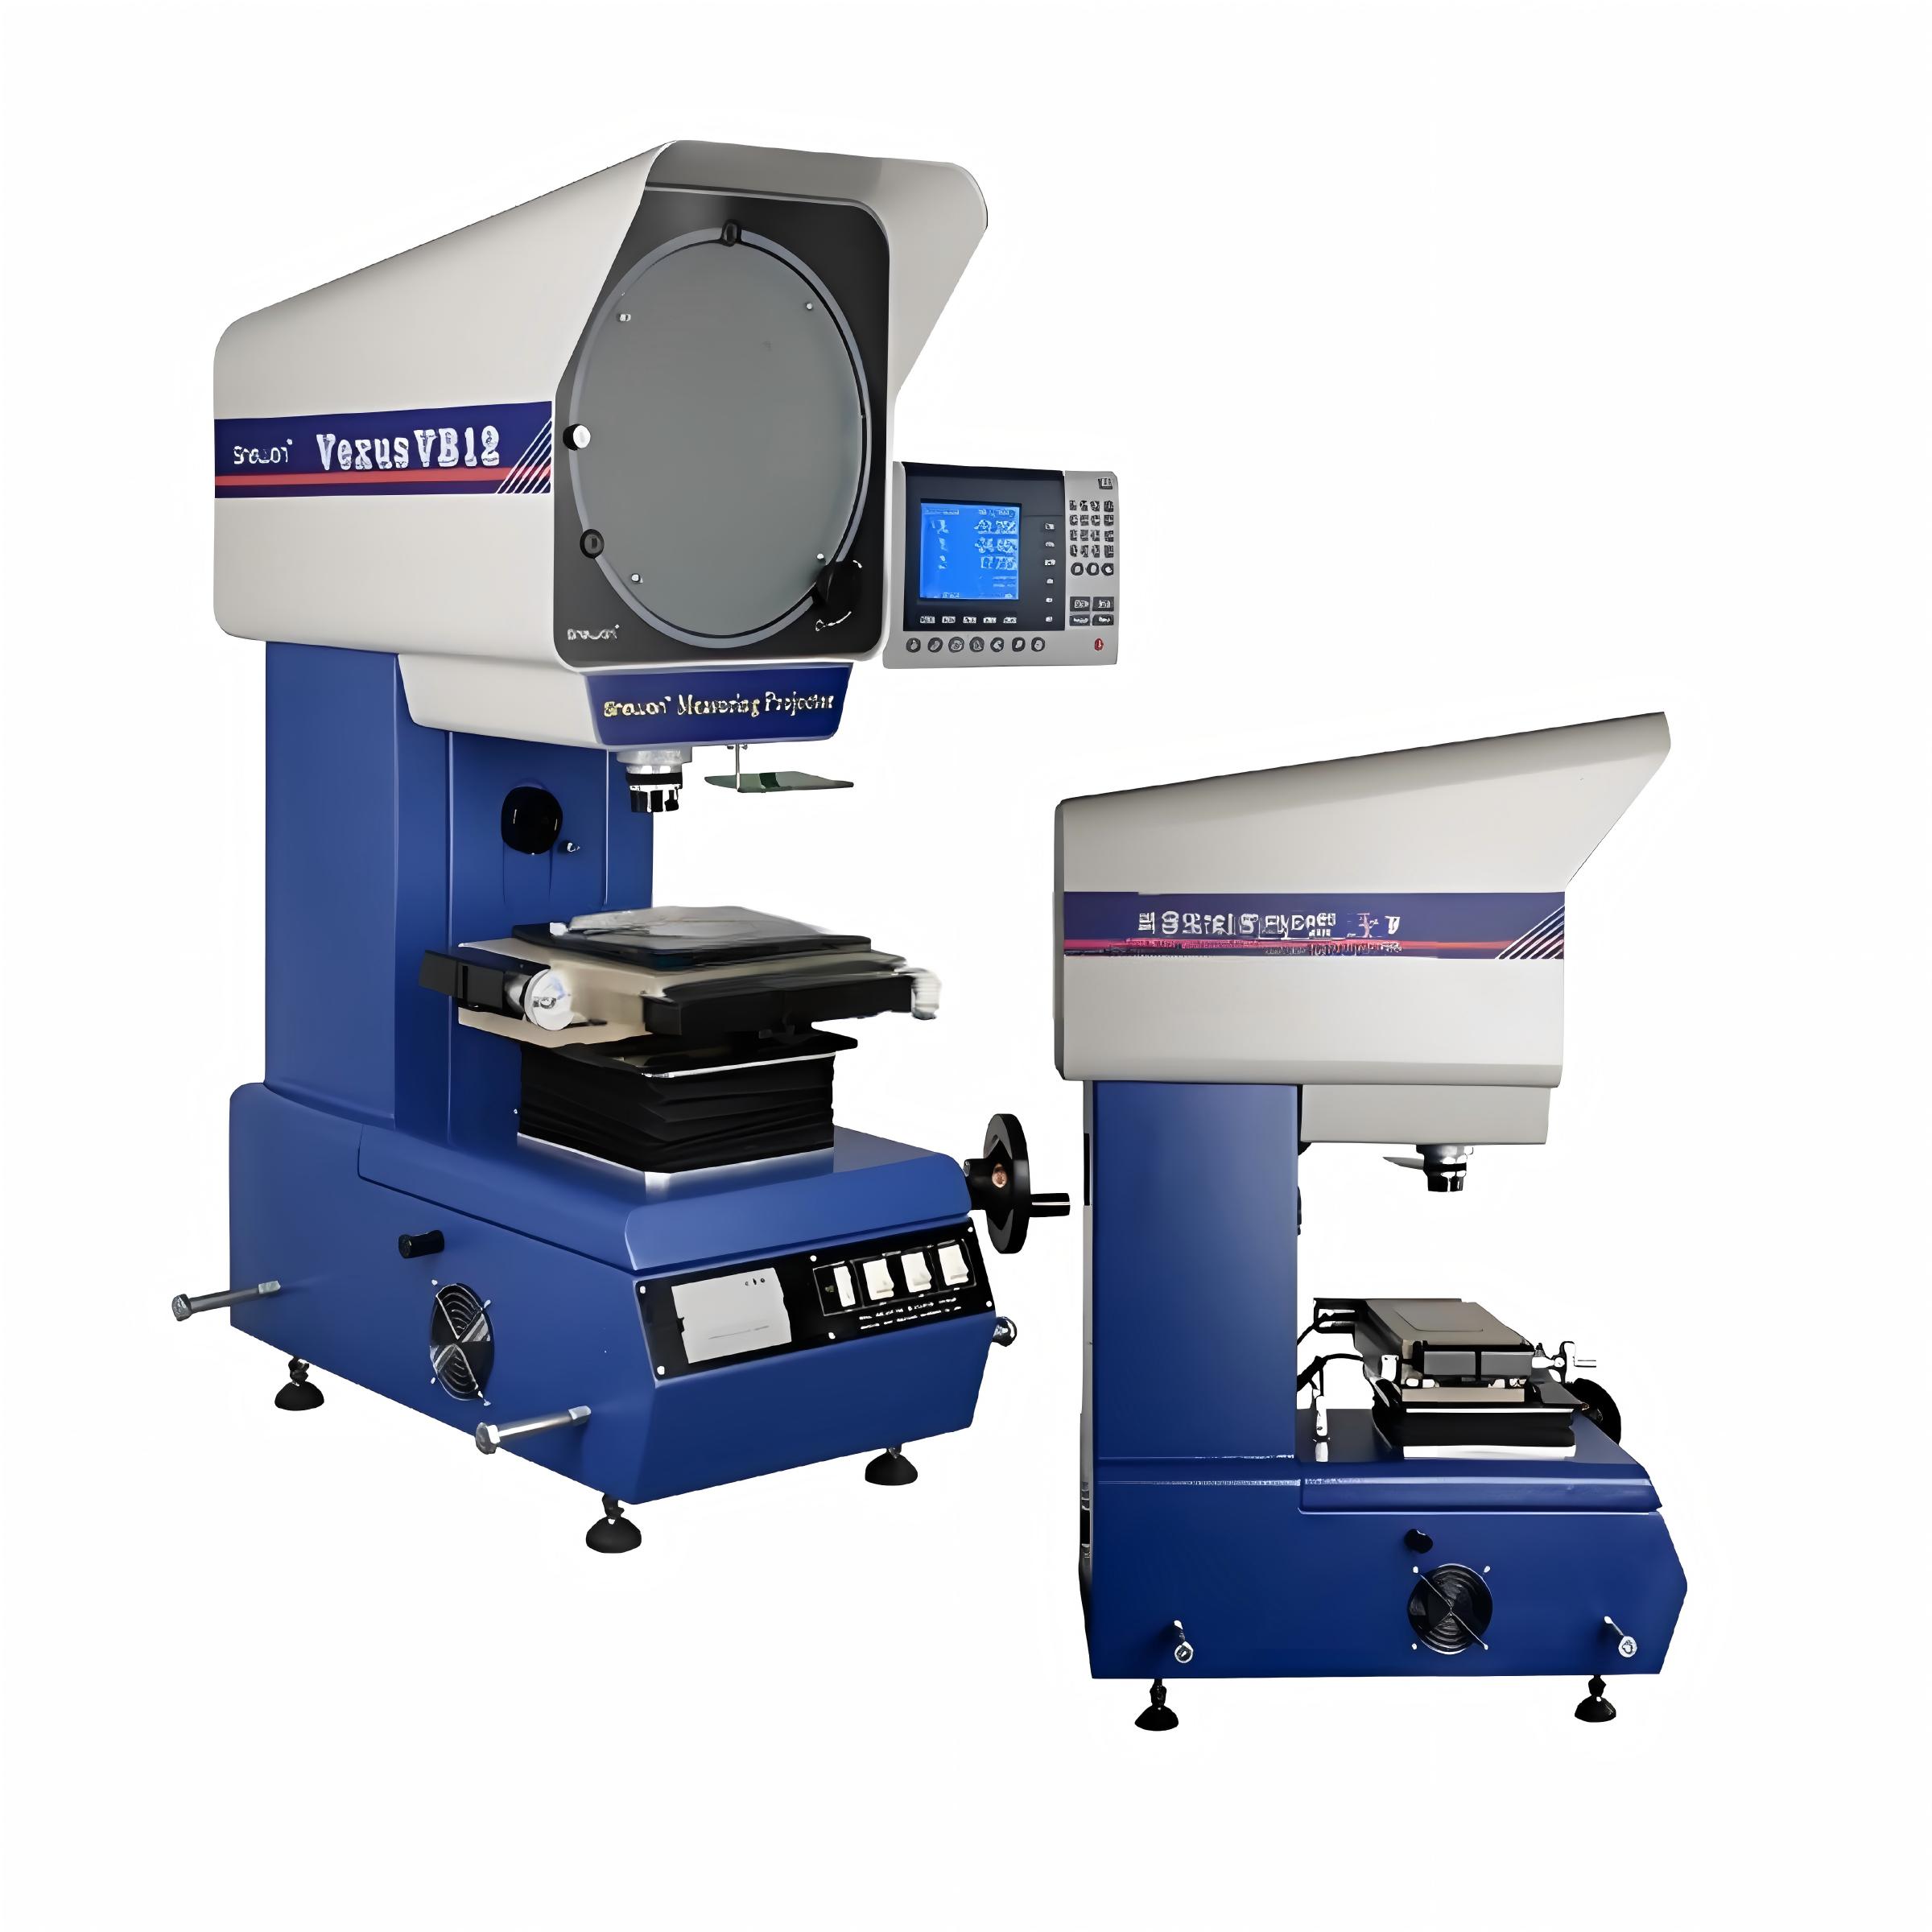
Most spec sheets parade a headline number—like a micron-level measurement—as if it were a promise. But that figure rarely survives contact with real workloads. The trap lies in treating a single isolated metric as the whole story. Thermal throttling, binning variances, and the specific test bench used to produce the number all stay hidden in footnotes, if they appear at all.
When you see a process node described in microns, it is not a uniform yardstick. Two products built on the "same" micron line can behave very differently because of transistor architecture, cache hierarchy, or memory controller choices. The spec sheet will happily list the best-case scenario, but it will not volunteer that the figure was achieved under a 20°C ambient with a golden sample.
To read between the micron lines, you need to ignore the bold print and hunt for the conditions. Look for sustained performance under load, not burst numbers. Compare how different vendors define "typical" or "maximum." A micron-sized gap on paper can translate into a much larger gap in your actual daily use, and the only reliable way to spot it is to test with the workload you care about.
Brightness, Contrast, and the Edges You Actually Need to See
Most screen calibration guides obsess over brightness and contrast as if they exist in a vacuum, but the real goal is far more practical: preserving the visibility of fine edges and subtle transitions that your work depends on. When brightness is cranked too high, the darkest steps of an image bleed together into a murky gray; when contrast is pushed too far, delicate highlight detail burns away to pure white. The trick is to treat both controls not as separate sliders to max out, but as a balancing act that keeps the boundary between two nearly identical tones just barely visible.
Start by lowering brightness until a true black patch on your test pattern no longer glows with a backlight halo, then raise it one notch so the first step above black is faintly distinguishable. From there, adjust contrast until a white patch stops blooming and retains a faint texture even at 95% luminance. This back-and-forth rarely lands where the spec sheet suggests, because every panel ages differently and every room has its own ambient light. What matters is that you can still count the individual strands in a dark fabric or the reflection on a wet street long after the automatic settings have given up.
The edges you actually need to see are rarely the obvious ones—they are the faint rim light around a portrait subject, the barely brighter sky behind a window frame, the single pixel of difference in a UI divider. If your monitor can't show those without squinting, no amount of internal processing or dynamic contrast will recover the information. Trust your eyes over the marketing numbers, run a grayscale step wedge, and make small adjustments over several minutes as your vision adapts. Once the edge between step 4 and step 5 is as clean as the edge between step 94 and step 95, you have found the only brightness and contrast settings that actually matter.
Stage Travel and Workholding: The Unsexy Specs That Matter
When evaluating a machine tool, buyers often gravitate toward spindle power or rapid traverse rates, but the real constraints on part size and setup flexibility hide in the travel limits and workholding interface. Stage travel defines the maximum envelope your tool can reach, and it’s rarely as simple as the X/Y/Z numbers on a spec sheet—overtravel, way covers, and cable management eat into usable stroke. If you plan to machine long shafts or deep pockets, you need to know the distance between the spindle nose and table, not just the nominal travel.
Workholding is equally unglamorous but far more consequential. A machine with generous travels becomes useless if the table slots, T-slot spacing, or fixture locating features don’t match your existing vises, chucks, or custom plates. The bolt pattern and clamping surface flatness decide whether you spend ten minutes or two hours on every setup. Cheap castings with poorly machined slots will frustrate even the most patient machinist, while a well-designed workholding grid lets you swap fixtures blind.
The unsexy specs also include way wiper quality, chip evacuation channels, and the location of the coolant return trough. These details don’t make the brochure cover, but they determine whether the machine stays accurate after a thousand cycles or slowly drifts out of tram. Before you get seduced by a flashy control pendant, lift the way covers and look at how the manufacturer handled the boring, critical interfaces between motion and clamping.
Lens Selection and Magnification Ranges Without the Upsell
Choosing a lens without the sales pitch starts with your most frequent subject, not the spec sheet. If you shoot small products or prints, a macro that gives you 0.5x to 1x at a comfortable working distance beats a zoom with a macro badge that only reaches 0.25x. For general walkaround work, a 35mm or 50mm prime often covers more ground than a slow 18-200mm superzoom, and you lose far less light.
The magnification range matters only in the band you actually use. A 24-105mm is fine for event work, but if you regularly need 1:1 reproduction, you will chase focus rings on a zoom that never quite gets there. Test the middle apertures and distances where you work, not the extremes shown in charts. Lenses are rarely at their best at both ends of the zoom range.
Skip the bundles that pile on filters, step-up rings, and cleaning kits you did not ask for. Buy the one focal length or zoom range that solves your current problem, then add another only when you hit a real limit. Two or three carefully picked lenses will cover almost any job without the upsell.
Day-to-Day Ownership: Calibration, Glass Care, and Real Costs
After the first week, you stop noticing the calibration settings and start trusting them. A decent colorimeter pays for itself the third time you don't have to reprint a batch of photos, but the real trick is rechecking every couple of months instead of chasing perfection daily. Ambient light shifts more than the panel does, so a quick profile update under your usual working lamp beats a midnight deep-dive into gamma curves.
Glass care is less about fancy sprays and more about what you don't do. Dry microfiber, light pressure, and never let a fingerprint sit overnight. The oleophobic coating wears down faster from harsh cleaners than from your fingers, so plain water on a damp cloth handles ninety percent of the mess. If you're using a stylus, a worn nib can scratch faster than a dirty screen, so swap tips before you blame the glass.
Real costs show up quietly: the extra electricity from leaving a bright panel on all day, the replacement cable that fails right after warranty, the anti-glare film that looked better in the listing. Budget for one mid-range accessory every year rather than a bag of cheap ones every season. That math has held up better than any spec sheet.
FAQ
A profile projector, often called an optical comparator, throws a magnified shadow of a part onto a screen so you can measure dimensions without touching the workpiece. You place the part on a glass stage, a light source projects its silhouette, and you compare that image against reference lines or use digital readouts to capture lengths, angles, and radii. It is especially handy for checking complex profiles, thread forms, and small stamped parts where contact probes might flex or damage delicate edges.
You will find them in tool and die shops, medical device manufacturing, automotive component inspection, and aerospace fastener production. Any place that needs quick verification of turned parts, gears, or injection-molded pieces without sending samples to a lab. They are also common in fastener plants to check thread angles and pitch diameters, and in electronics for connector dimensions.
Screen size matters less than optical quality and magnification range. For tiny features, you want at least 10x and 20x lenses with good edge definition, a surface illumination option (not just profile lighting), and a stable stage with fine adjustment. Digital readout resolution of 0.001 mm or better helps. Also check that the lens working distance gives enough clearance for fixtures or holding small parts.
Older units relied on eyeballing a shadow against a chart or using vernier handwheels, which left room for operator bias. Digital systems give direct X-Y coordinates, store measurement points, and often compute circles, slots, and angles automatically. That does not eliminate skill, it just removes a lot of manual arithmetic and transcription errors, and makes repeatability much easier to document.
One big one is not allowing the machine and part to reach a stable temperature before measuring. Another is trusting a worn or dirty screen or a scratched chart overlay. People also focus too heavily on the edge of the shadow without checking surface illumination alignment, so a burr or chamfer gets misread as the true edge. And many skip regular calibration because the image on the screen still seems acceptable.
Keep the glass stage clean with a lint-free cloth and a non-abrasive cleaner, and inspect it for chips. Blow off dust that settles inside the lamp housing, and replace bulbs before they blacken too much. Check the focusing mechanism for smooth travel, and verify digital scales against a certified glass scale or gauge block every few months. If the projector has a fan or ventilation holes, keep them clear to avoid heat drift.
For many 2D silhouettes and simple height differences, yes, it is faster and cheaper to operate. But it will not give you full 3D surface data, deep-hole measurement, or automated scanning of complex geometries. Shops often keep a projector at the machine tool for quick spot checks and reserve the CMM for final inspection or parts with tight 3D tolerances. They complement each other rather than compete.
The projected edge you measure is only as sharp as the light source. A slightly misaligned lamp or a failing bulb can blur the boundary and shift your readings by tens of microns. Properly collimated light with the right condenser setting gives a crisp black-to-white transition. For surface features like steps or blind holes, you need oblique or coaxial illumination, otherwise you are measuring a shadow that does not match the actual geometry.
Conclusion
A profile projector earns its keep only when it fits the way you actually measure. Bench space is the first filter: a bulky chassis that crowds out your height gage or leaves no room for a fixture becomes a daily annoyance, no matter how impressive the brochure looks. The real story hides in the spec sheet—stated resolution and repeatability often assume ideal conditions that your shop floor never sees. You have to read between the micron lines and ask what happens after the machine warms up or the stage gets a little wear. Brightness and contrast matter more than raw magnification because a washed-out edge forces you to second-guess every reading. Stage travel and workholding are the unsexy specs that decide whether you can measure an actual part without building a custom clamp. If the travel is too short, you spend half your time repositioning; if the workholding is flimsy, your measurements drift before you notice.
Lens selection should be driven by the part features you need to resolve, not by the upselling of extreme magnifications that you will rarely use. A 10x lens that gives a crisp, flat image beats a 50x lens with blurry edges and a shallow depth of field. Think about the range of sizes you will encounter and pick the two or three lenses that cover that range without constant swapping. Day-to-day ownership is where the real costs pile up: calibration intervals, replacement glass for the screen, and the time lost when a lens gets knocked out of alignment. Profile projectors are mechanical and optical workhorses, but they demand attention. The ten machines worth your bench space are not the ones with the longest feature list—they are the ones that stay accurate, stay bright, and stay out of your way over years of daily use.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/